Constructed from high-tensile weathering Corten steel and structural I-beams. Choose from ready-to-ship ISO platforms or custom modular configurations with turn-key utility integration.
Strategic guidance for procurement managers, construction logistics directors, and modular housing developers evaluating mobile asset acquisitions.
Modern global logistics and decentralized capital projects require robust on-site storage and rapidly deployable infrastructure. Selecting a top-tier mobile storage unit factory and exporter is no longer a transactional purchase of steel boxes; it is a critical strategic decision impacting operational uptime, security of high-value tools, and personnel safety. As industrial sectors face volatile weather conditions, tighter project schedules, and strict workplace standards, standardized intermodal units have evolved into highly engineered, multi-purpose modular assets.
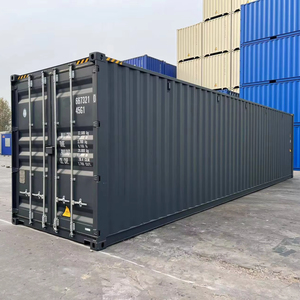
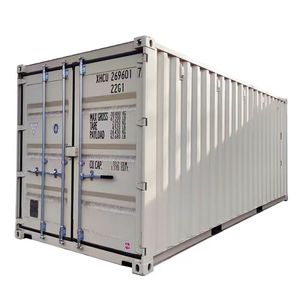
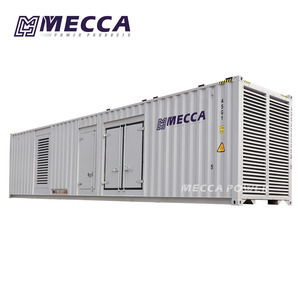
Historically, mobile storage relied on retired secondary market containers prone to structural fatigue, compromised corner castings, and floor delamination. Today, Tier-1 manufacturing facilities produce purpose-engineered Corten steel storage solutions characterized by superior yield strength (SPA-H grade), marine-grade multi-layer epoxy coating systems, and precision robotic welding. Whether specifying 20ft side-opening units for rapid equipment turnaround or 40ft High Cube containerized power generation enclosures, sourcing factory-direct eliminates intermediary markups and guarantees verifiable material test reports (MTRs).
Delivering institutional-grade industrial fabrications with certified weld traceability and end-to-end quality governance.
Anticipating engineering, logistics, and sustainability transformations across the 2025–2030 commercial landscape.
The procurement profile for relocatable mobile units is shifting toward hybrid multifunctionality. Organizations are moving away from passive metal shells toward dynamic, self-sustaining modular units. Leading international buyers prioritize three primary procurement vectors:
1. Turnkey Decentralized Energy & Climate Adaptation: As mining, renewable energy sites, and civil engineering projects move into remote areas, demand for containerized generator plant housing (such as the Cummins 2500kW heavy-duty diesel unit) and factory-installed thermal break insulation has grown. Modern storage units increasingly incorporate pre-installed electrical conduits, explosion-proof exhaust louvers, and HVAC brackets straight from the assembly line.
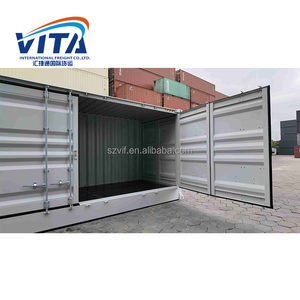
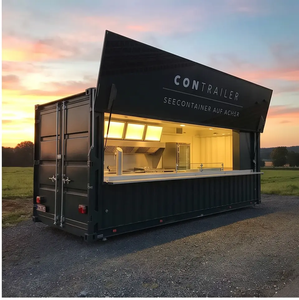
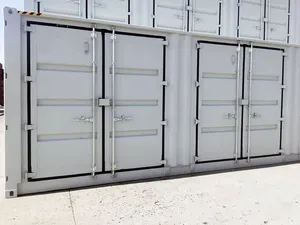
2. Biophilic and Architectural Repurposing: Reusable space designs are becoming standard. Buyers are combining basic dry storage footprints with functional worker welfare facilities. Open-side full-access 20ft and 40ft units now frequently serve dual roles as secure inventory vaults during the week and modular pop-up operational hubs or dining mess halls on weekends, as seen in custom container cafe-bar platforms.
3. Scope 3 Carbon Reductions via Modular Longevity: Institutional ESG mandates now favor standardized ISO modular units over light-gauge, short-life temporary sheds. Standardized container architecture provides salvageable value after project decommissioning. Units can be easily loaded, shipped, re-outfitted, and deployed to new sites multiple times, reducing material waste.
Clear answers to frequent technical, logistical, and structural engineering questions raised during corporate RFP evaluations.
We use genuine Corten-A / SPA-H anti-corrosion structural steel for all corner posts, top/bottom side rails, and corrugated paneling. Floor structures incorporate hot-rolled C-channel or I-beam crossmembers lined with 28mm marine-grade hardwood plywood or optional anti-skid checkered steel plates.
Our 20ft and 40ft open-side storage units feature reinforced top header beams and thickened corner posts that exceed standard ISO deflection limits. This engineering supports maximum top-lift gross weight ratings without bowing, even during dynamic ocean transit.
Every unit undergoes SA 2.5 standard shot-blasting to remove mill scale, followed immediately by a zinc-rich epoxy primer (30–40μm), an epoxy intermediate barrier coat (40–50μm), and a durable polyurethane or acrylic topcoat (40–50μm), yielding a total Dry Film Thickness (DFT) over 120μm.
Yes. We deliver custom builds directly from the production line, including custom heavy equipment mounts, acoustic attenuators, fire-rated insulation, intake louvers, and distribution panels, helping you avoid costly post-delivery retrofits on-site.